IoT & Industry 4.0 Solutions
IoT & Industry 4.0 Solutions
Our IoT and Industry 4.0 solutions connect machines, systems, people, and production environments through a unified digital ecosystem. By bringing together real-time dashboards, cloud-based monitoring, energy intelligence, and remote diagnostics, we give businesses greater visibility into their operations and the information needed to make timely, informed decisions.
Secure connectivity and intelligent data processing help organisations monitor equipment performance, identify operational trends, and respond to potential issues before they affect production. Our scalable IoT architecture is designed to support evolving industrial requirements while maintaining reliable communication across connected assets.
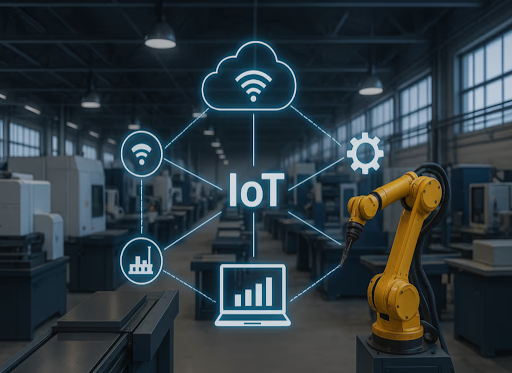
From tracking equipment health and production performance to analysing energy consumption, we help manufacturers move beyond conventional operations and build connected, efficient, and future-ready facilities aligned with Industry 4.0.
Next-Generation IoT Solutions for Smart Manufacturing
Real-Time Machine & Production Monitoring
Monitor machine parameters, production-line efficiency, alarms, and performance indicators in real time for greater control over your operations.
Secure Cloud Connectivity
Transfer machine and operational data securely to cloud platforms, enabling advanced analytics, remote monitoring, and better access to critical insights.
Connected Machine Communication
Create seamless communication between machines, PLCs, controllers, and industrial systems to support a more integrated and responsive production environment.
Security Built into Every Connection
Protect industrial data with secure communication protocols, encrypted data transmission, and dependable device connectivity across your connected infrastructure.
Frequently Asked Questions
1. What are IoT and Industry 4.0 solutions?
IoT solutions connect machines, sensors, and industrial systems to collect and share operational data. Industry 4.0 uses this connectivity to improve automation, production visibility, and data-driven decision-making across manufacturing operations.
2. How can IoT solutions improve manufacturing efficiency?
IoT solutions provide real-time insights into machine performance, production activities, and equipment health. These insights help businesses identify inefficiencies, reduce downtime, and make informed decisions to improve overall operational efficiency.
3. What is real-time machine and production monitoring?
Real-time monitoring allows businesses to track machine parameters, production-line performance, operational alarms, and key performance indicators. It helps teams identify issues quickly and maintain better control over manufacturing processes.
4. What types of data can IoT systems collect from industrial equipment?
IoT systems can collect data such as machine status, production counts, equipment temperature, energy consumption, operational alarms, and performance indicators. This information helps manufacturers understand equipment behaviour and identify opportunities for improvement.
5. Can IoT solutions integrate with existing machines, PLCs, and industrial systems?
Yes, IoT solutions can be designed to communicate with compatible machines, PLCs, controllers, and industrial systems. Integration depends on the equipment, communication protocols, and existing infrastructure.
6. How does cloud connectivity benefit industrial operations?
Cloud connectivity enables industrial data to be accessed, stored, and analysed through connected platforms. It supports remote monitoring, advanced analytics, and convenient access to operational information from authorised locations.
7. Are IoT and Industry 4.0 solutions secure?
IoT solutions can incorporate security measures such as encrypted data transmission, secure communication protocols, and controlled device connectivity. The overall security level also depends on system configuration, network protection, and ongoing maintenance.
8. Can businesses monitor industrial operations remotely using IoT?
Yes, connected IoT platforms can allow authorised users to access real-time operational data, view dashboards, and monitor equipment remotely. This improves visibility across production environments without requiring users to be physically present on the factory floor.
9. Are IoT solutions suitable for businesses with expanding production requirements?
Yes, scalable IoT architectures can support additional machines, devices, data sources, and production locations as business needs evolve. The extent of expansion depends on the existing infrastructure and the design of the IoT solution.
10. What are the main benefits of implementing Industry 4.0 solutions?
Industry 4.0 solutions help businesses improve production visibility, monitor equipment performance, analyse energy consumption, identify operational issues, and make faster decisions. These capabilities support more efficient, connected, and future-ready manufacturing facilities.
Ready to get started?
Get in Touch
We’d love to resolve your queries with personalised assistance.